Industrial Cleaning Chemistry Engineered For Refinery Operations

Indie Chem Co helps refineries, petrochemical plants, and terminals solve their toughest operational problems — from underperforming units and heat exchangers to the most demanding decontamination and turnaround cleaning challenges — through process-matched chemical application programs.

Scroll

70+ Years Field Experience

Chemistry programs developed by refining industry veterans

Serving Major Gulf Coast Refineries

Gulf Coast-based, serving customers nationwide

Chemistry Matched to Your Process Conditions

No generic formulations — every program is application-specific

No Off-the-Shelf Solutions

Custom-engineered for your unit, feedstock, and timeline

What We Deliver

Engineering-driven solutions that restore performance, cut waste, and make refinery turnarounds safer and faster.

We keep equipment in its operating envelope longer, recover more product from residues, and execute cleaning with less water, less waste, less vapor exposure, and fewer planned entries.

Industrial cleaning is too critical for generic chemistry, which is why every treatment program is engineered by industry veterans who tailor solutions to your assets, operating conditions, and your fouling mechanisms.

The result is safer operations, faster turnarounds, and longer run lengths between cleanings — all aligned to your specific performance goals.

Why We Exist

Zero downtime is the only standard.

Every hour a refinery sits idle costs more than most businesses earn in a month. Indie Chem Co exists to make unplanned downtime a thing of the past — pairing field-proven cleaning chemistry with hands-on engineering support so critical systems keep running under the harshest conditions.

We're built on old-school values: engineering, integrity, and real-world performance.

What We Do

Unit-specific treatment programs that decontaminate, degas, and clear safely.

See all services

Refinery Unit Fouling Mitigation & Removal

Purpose-formulated application treatment programs for crude unit towers, desalters, FCC units, hydrotreaters, reformers, cokers, and more. We address pyrophoric hazards, hydrocarbon decontamination, and deposit removal via data-driven analysis and solutions, to bring your units in safely and on schedule.

Learn More

Heat Exchanger Fouling Mitigation & Removal

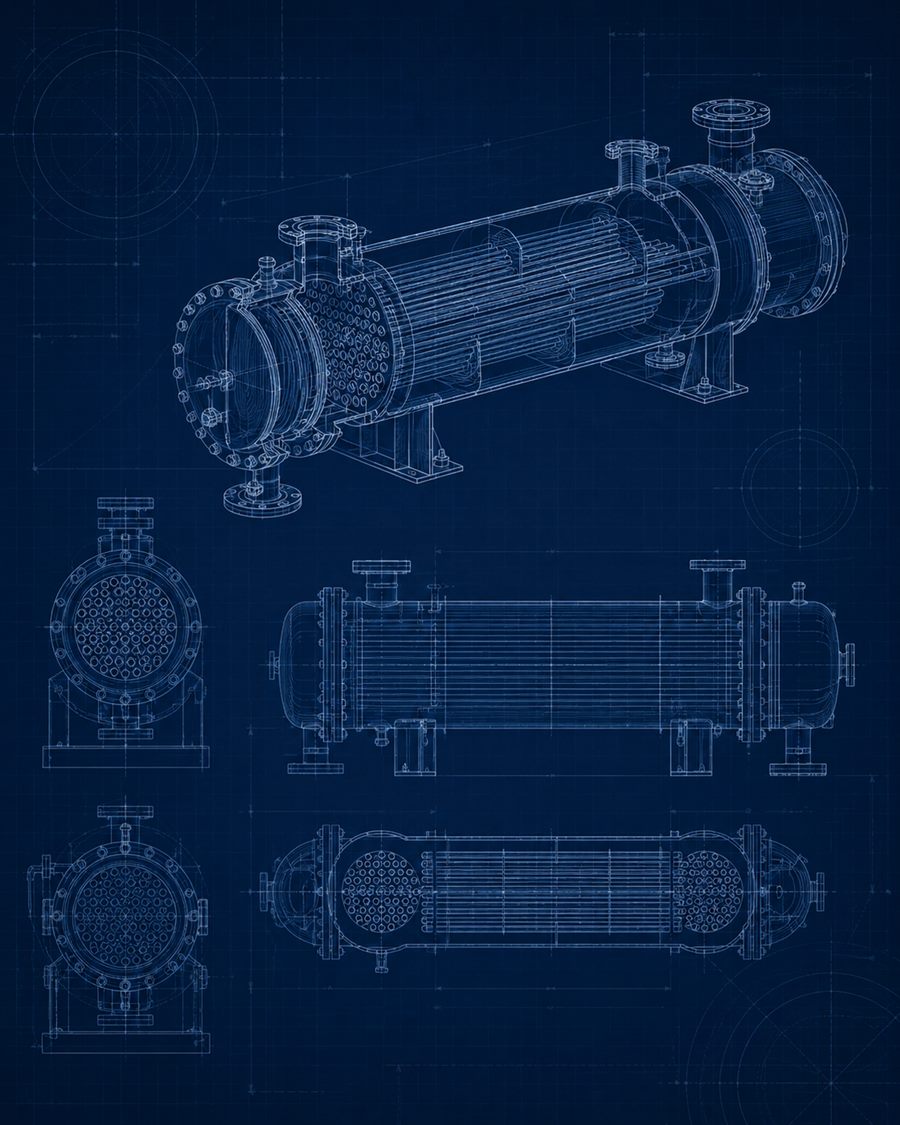
Organic deposits, inorganic scale, salts, coke, and polymer fouling all degrade heat transfer efficiency, drive up operating costs, and decrease throughput. Our treatment programs are matched with your heat exchanger design, crude grade, operational data, and fouling type through careful diagnosis of deposit analysis.

Learn More

Tank Cleaning & Turnaround Chemistry

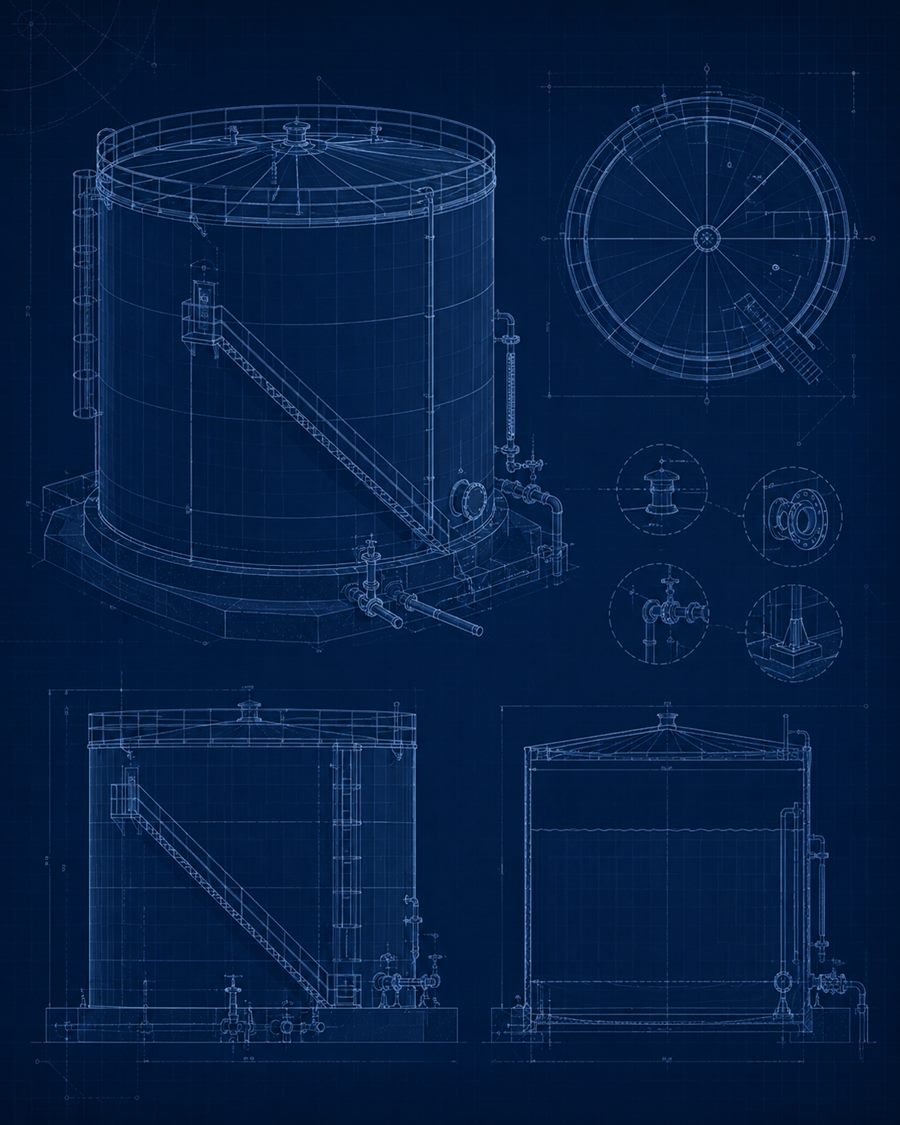
Accumulated sludge bottoms and product heel buildup reduce usable capacity and pose challenges for tank cleaning and entry before API inspection. Our in-tank chemical treatment programs reduce sludge volume, improve pumpability, reduce asset OOS timelines to support your LPO, and help provide safe entry, minimizing manual cleaning time and confined space exposure.

Learn More

Our Story

Built by engineers.
Tested in the field.

Indie Chem Co was founded on a simple frustration: too many chemical suppliers sell products they've never run in a live plant. We do the opposite.

Every program we offer is grounded in engineering, proven under real operating conditions, and backed by people who've stood on the platform when it counts.

Premium chemistry. Real-world performance. No compromises.

Industries We Serve

Built for the toughest industrial environments.

01

Refineries

Crude unit decontamination, turnaround chemistry, and ongoing fouling control for atmospheric and vacuum distillation, conversion, and treating units.

Learn More
02

Petrochemical Plants

Process cleaning chemistry for ethylene crackers, polymer facilities, and specialty chemical operations where process contamination and fouling directly impact product quality and yields.

Learn More
03

Storage Tanks & Terminals

Sludge and gas reduction, waste minimization, product displacement, and tank preparation chemistry for crude storage and product tanks at terminals and storage facilities.

Learn More

Why Work With Us

The trusted technical partner that knows your operation.

Application Treatment and Chemistry Matched to Process Conditions

Effective industrial cleaning programs are not interchangeable. The application treatment plan, the fouling type, operational temperatures, metallurgy and downstream constraints are all factors that can and should be addressed to build a cost-effective, data-driven strategy. We conduct a technical review of your specific conditions before recommending any program.

Long-Term Customer Relationships

We don't operate on a transactional model. Our customers typically work with us across multiple turnaround cycles and ongoing maintenance programs, because consistency in chemistry selection and field knowledge directly improves outcomes over time. When we know your unit, we bring that institutional knowledge to every job.

Operational Outcomes, Not Just Products

We measure our performance by your results — safe unit entry, schedule adherence, restored heat transfer efficiency, reduced sludge volume, and extended run length. Product delivery is a means to those ends, not the goal in itself.

Responsive Technical Support

Shutdowns and turnarounds don't pause and wait for slow responses. When conditions change in the field — different deposit composition, unexpected fouling, schedule compression — we are reachable and ready to adjust. Our technical team supports active programs and answers questions from your operations and maintenance personnel directly.

Ready to solve your most challenging problem?

Tell us about your unit, your timeline, and your challenge. We'll come back with a technically grounded recommendation from a real human — not an automated product catalog or AI chatbot.

Request a Treatment Recommendation